Capabilities
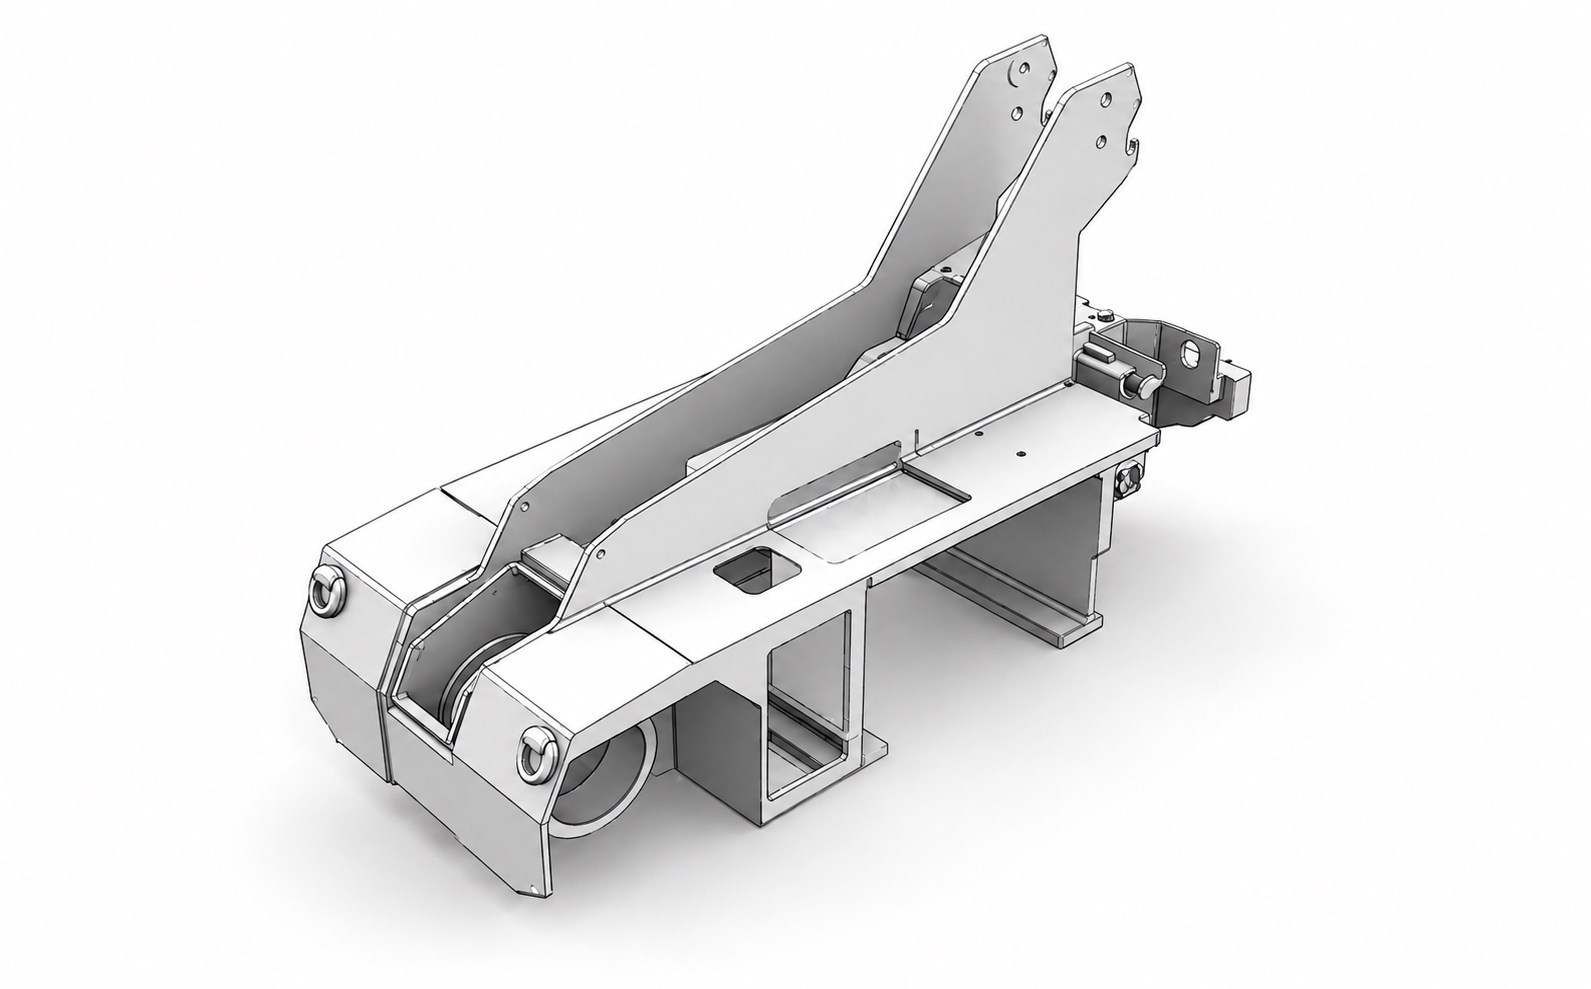
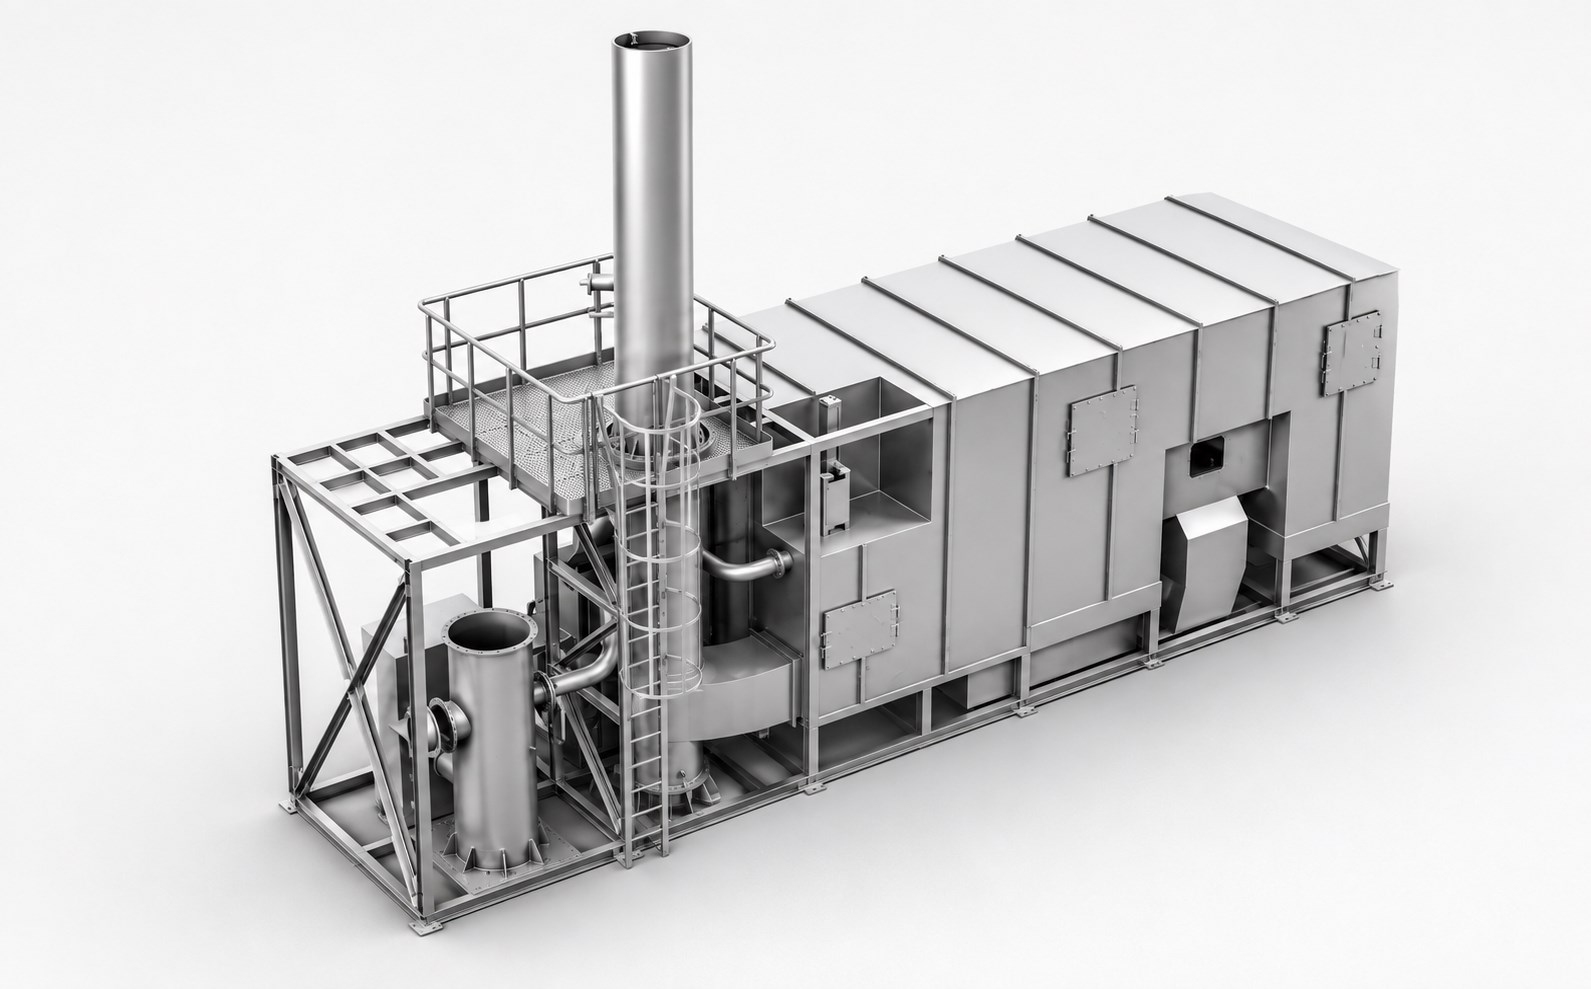
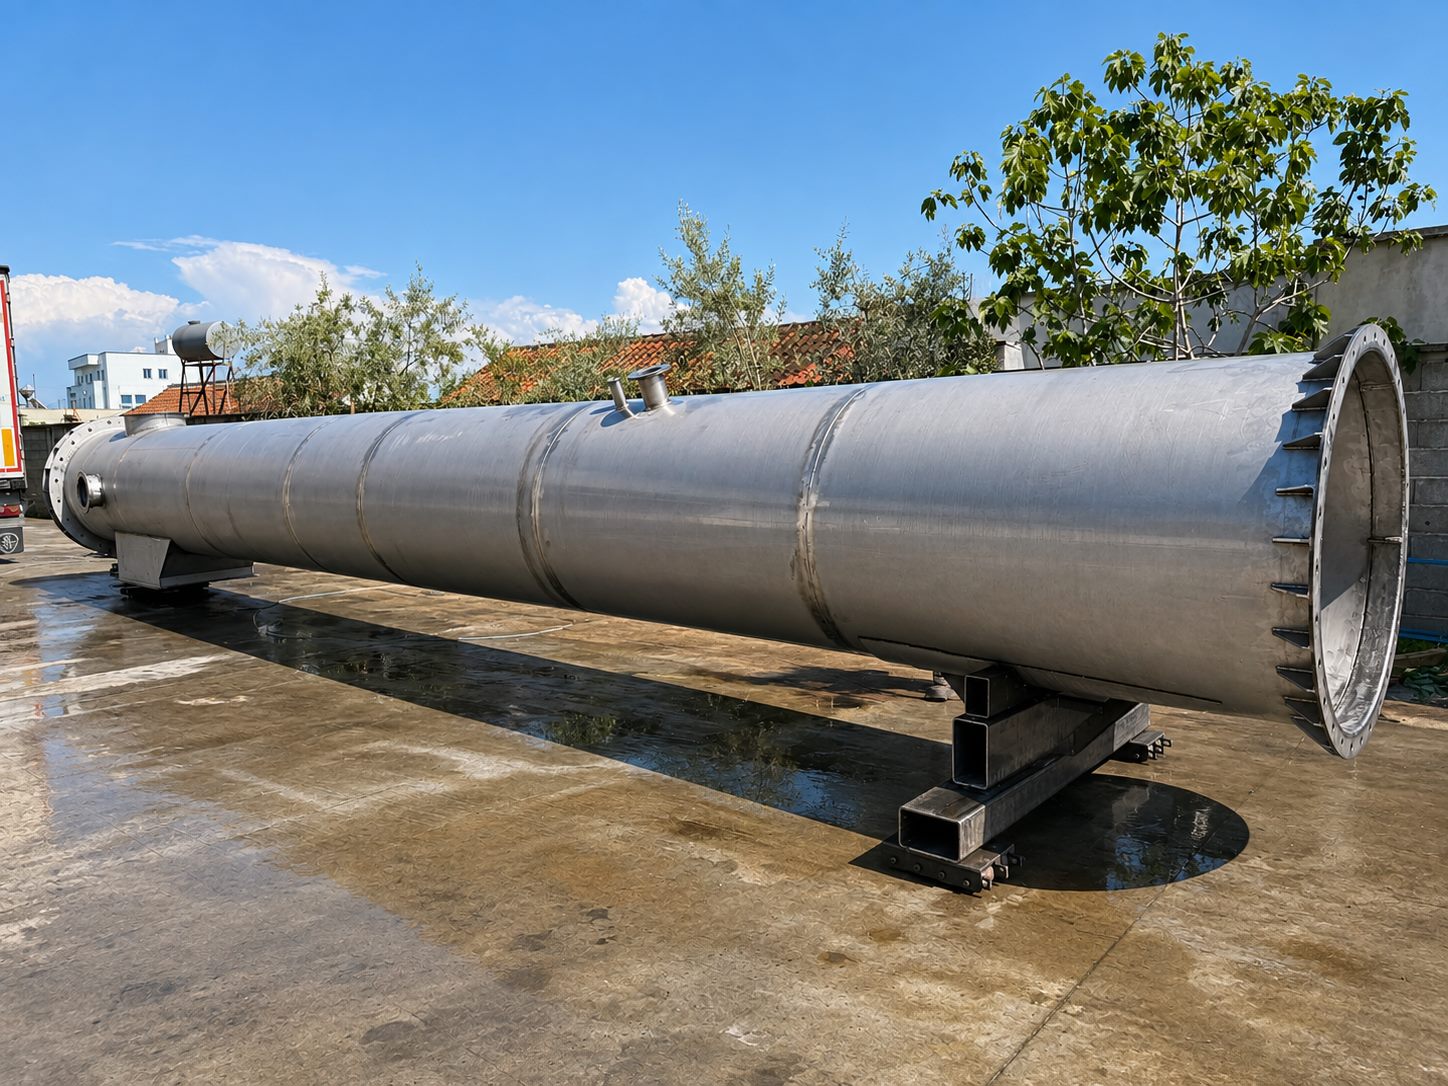
Everything happens under one roof.
Cutting, forming, joining and finishing on the same floor. Nothing is subcontracted, so nothing waits on someone else's queue.
CO₂ laser cutting
Flat parts cut straight from your DXF, with no tooling cost and no setup delay on revisions. Clean, square edges through the full thickness range.
- Machine
- Bystronic Bystar 4020
- Source
- 3.0 kW CO₂
- Bed
- 4000 × 2000 mm
- Mild steel
- to 16 mm
Plasma cutting
Heavy plate and long structural parts on a ten-metre bed — where the laser's capacity stops, this starts. True Hole produces bolt-ready holes in mild steel without a second operation.
- Machine
- Gemini 254 PG
- Source
- Hypertherm HPR260XD
- Bed
- 10 000 × 2500 mm
- Mild steel
- to 38 mm
Sawing
Stock cut to length on an automatic numerically controlled cycle, ahead of the forming and welding bays.
- Machine
- Thomas DC 420
- Cycle
- Ciclomatic CN
CNC bending
Bend allowance, inside radius and springback are solved before the tool touches steel, so the first part is the good part.
- Machine
- Bystronic Beyeler PR
- Press
- 500 t / 5000 kN
- Length
- 4100 mm
- Axes
- 8
Welding
MIG and TIG on steel, stainless and aluminium. Sequence and heat input are planned to hold geometry true across the assembly.
- Process
-
- Pulsed MIG (GMAW-P)
- MIG/MAG, FCAW
- Stick / MMA
- TIG, TIG pulse
- Arc gouging (CAG)
- Wire
- 0.8–1.2 mm
Finishing
Welds ground back, edges deburred, surfaces prepared and coated. Done properly, none of the work is visible in the finished part.
- Prep
- P60 → P120
- Roughness
- Ra ≤3.2
- Coating
- Powder, 80 µm
- Colour
- Any RAL